Hey everyone, it’s Jake here—part of the engineering team over at the Mill-Turn shop, and let’s be real, when people ask me what the biggest headache is for new Mill-Turn owners, it’s not the complex multi-axis programming or the fancy syncing between milling and turning heads. It’s the lubrication. I’ve seen so many shops drop the ball on this, and end up with costly downtime, burned-out bearings, or even a whole head replacement way sooner than it should be. Today, I’m breaking down exactly what you need to get right for your Mill-Turn machine’s lube needs—no stuffy jargon, just real stuff I’ve actually seen play out in our own customers’ shops. Mill-Turn Machine Machine
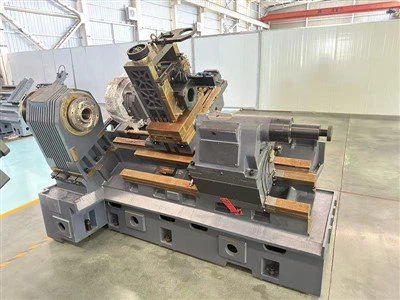
First off, let’s get one thing straight: Mill-Turn machines aren’t just mills that do turning, or lathes that do milling. They’re a hybrid—two totally different motion systems (rotating milling heads, rotating work spindles, linear axes for both) crammed into one setup. That means their lubrication needs aren’t one-size-fits-all, and if you use generic oil just because “it works for my old lathe,” you’re asking for trouble. I once had a customer bring in a 3-year-old Mill-Turn that the previous owner used standard hydraulic oil for the linear guides. The guides were shot in 2 weeks—turned out hybrid machines have way more dynamic load on every component than a standalone lathe or mill. Let’s break each key component down, ‘cause that’s where it gets specific.
Starting with the big ones: the spindle system. Both the main turning spindle (where you chuck your workpiece) and the milling head spindles (the ones with the end mills, drills, etc.) are high-tension, high-speed parts on Mill-Turns. I’m talking turning speeds up to 5,000 RPM for the main spindle, and milling heads hitting 15,000 RPM or more. What lube do these need? It’s not just oil—most modern Mill-Turns use grease for the rolling element bearings inside the spindles, and not just any grease. It has to be a synthetic, high-temperature, low-wear grease with extreme pressure (EP) additives, but not too much EP—wait, right, too much EP can actually corrode the bearing seals over time, which lets dirt in. We recommend a lithium-complex or polyurea-based grease for 90% of our machines, and if you’re running really high temp operations (like machining stainless or titanium that generates tons of heat), go with a synthetic polyglycol-based grease—it handles the heat way better. And don’t over-grease! I see this all the time—shops pump so much grease in that it builds up heat itself, causes friction, and eventually burns out the spindle. The manual will tell you the exact amount, but if you hear squealing from the spindle during a fresh grease job, you put too much.
Next up: linear axes. Mill-Turns have linear rails and ballscrews for the X, Y, Z axes (and sometimes B or C axes for multi-tasking), and these take a brutal beating. You’re not just moving one direction—you’re switching between milling along the Y axis and turning along the Z axis, all while loaded up with a heavy workpiece. For linear rails, most Mill-Turn suppliers (that’s us, fyi) use either oil mist lubrication or automatic grease dispensing systems. Wait, why not just manual grease? Manual is fine for old lathes, but when you’re moving axes 10 times a minute, day in and day out, you need consistent, controlled lubrication. Oil mist works great for high-speed linear systems, ‘cause it coats every part evenly, but you have to make sure the mist system is calibrated—too much oil builds up on the machine walls, too little leads to wear. Grease is simpler for lower-speed linear axes, but make sure it’s a high-viscosity grease for heavy loads, not the thin stuff you’d use for a door hinge. For ballscrews specifically—they need a different lube than linear rails. Ballscrews have tiny recirculating balls that rely on lubrication to keep them rolling smooth, not grinding. We use a synthetic gear oil for ballscrews, viscosity grade 220 usually, but check your machine’s load rating—if you’re running 10,000 lb workpieces, bump that up to 320.
Then there’s the axis gears and rotary tables, especially for multi-tasking Mill-Turns with C and B axes that rotate while you’re machining. These are often overlooked ‘cause people fixate on spindles and linear rails, but they take a ton of cyclic load. For these, automatic oil circulation systems are your best bet. They pump clean, filtered oil through the gear housing, which not only lubricates but also cools the gears from the friction of constant rotation and load changes. The oil here needs to have good anti-foam additives too—if the oil foams up, you’re not getting consistent lubrication, and that leads to pitting on the gear teeth. I had a customer who skipped the oil filter change on their rotary table gears, and a tiny metal shard got caught in the lube line, scratched the gear, and they had to replace the whole table for $12k. Ouch. That’s the kind of stuff you avoid by sticking to the right lube and maintenance.
Wait, let’s talk about the dirty lube stuff—contamination is the #1 killer of Mill-Turn lubrication systems. You can use the best lube in the world, but if there’s metal shavings, coolant, or dirt in it, you’re screwed. Mill-Turns produce a lot more chips than standalone mills or lathes ‘cause you’re doing both operations at the same time. Chips can get into the lube lines, or even mix with grease if the seals fail. That’s why every modern Mill-Turn should have lube filtration systems—we install 10-micron filters on all lube circuits for our machines, and some of our higher-end models have 5-micron filters for high-precision axes. Also, you have to change the lube regularly, but not on a one-size-fits-all schedule. If you’re machining mild steel all day, you can go longer between lube changes than if you’re machining Inconel or titanium, which generate more heat and more fine metal shavings. Our recommendation: check the lube viscosity every 3 months, and change it if it’s thicker than it should be (heat breaks down oil, makes it thicker) or has visible contamination.
Another thing people mess up: mixing different lubricants. I’ve seen guys dump old grease from a lathe into their Mill-Turn’s spindle, or mix two different gear oils ‘cause they ran out of the right one. Don’t do that. Synthetic greases and oils have different chemical bases—mixing them can cause them to break down, form sludge, or even corrode metal parts. If you have to top off and you’re not sure, call your supplier (that’s us) or check your machine manual. We include a quick reference card with every machine that lists exact lube types for every component, no guesswork.
Oh, and let’s not forget about the auxiliary systems—like the spindle cooling unit and the way you route lube lines. Wait, the cooling unit is tied to lube, right? Spindles run hot, especially when you’re doing high-speed milling, and if the lube doesn’t keep them at the right temp, the spindle expands, throws off your tolerance, and wears out faster. Most Mill-Turns have a lube cooling circuit, so you need to make sure that’s maintained too—change the coolant in the cooling unit regularly, same as you do for the machine. Also, lube lines shouldn’t be routed near hot parts, like the main spindle motor. If a lube line gets too hot, the oil or grease breaks down before it even gets to the component it’s supposed to lubricate. We test all our lube line routes during machine assembly to avoid that, but if you’re retrofitting or modifying a used Mill-Turn, double-check that.
Wait, let’s use a real example to drive this home. Last year, we sold a new Mill-Turn to a shop that had been using old, generic lube for their 10-year-old hybrid machine. They switched to the lube specs we recommended, and their spindle downtime went from once every 6 months to once every 2 years. Their linear rail wear dropped by 70%, and they even increased their cutting speeds by 10% ‘cause the machine ran smoother, no more hesitation from dry guides. That’s the payoff—get the lube right, and your machine doesn’t just last longer, it performs better.
I know, I know, this sounds like a lot to track, but it’s not rocket science. The key is to stop treating your Mill-Turn like a single-function machine and start treating each of its hybrid components (spindle, linear axes, gears) as separate systems with unique lube needs. Don’t cut corners on lube— that $50 bucket of synthetic grease for spindles is way cheaper than the $5,000 spindle replacement you’ll need if you skip it. And don’t forget maintenance: check lube levels daily (most machines have a quick sight glass), change filters every oil change, and schedule lube fluid changes based on your actual workload, not a generic calendar.
If you’re still confused about what lube your specific Mill-Turn needs, or you’re looking for a new machine that’s designed with these lube systems built right (no shoddy line routing, correct filtration, and component-specific lube specs pre-loaded), hit us up. We work with shops of all sizes, from small job shops to large production facilities, to make sure their Mill-Turns run smooth, no lube-related surprises.
Wait, before I wrap up, let’s list a quick cheat sheet for anyone taking notes:
- Spindles: Synthetic polyurea/lithium-complex grease, high temp, EP-balanced, not over-grease.
- Linear guides: Automatic grease/oil mist, controlled application, not manual grease for high-use.
- Ballscrews: Synthetic gear oil, viscosity grade matched to machine load.
- Gears/rotary tables: Circulating oil, anti-foam additives, regular filtration.
- Non-negotiables: 5-10 micron lube filters, no mixing lubricants, regular contamination checks.
Look, I’ve been around Mill-Turns long enough to know that lube is the unsung hero of reliable operation. You can have the fanciest multi-axis programming, the tightest tolerances, the fastest tool changers, but if your lube system is garbage, your machine is garbage. Don’t be the shop that blames the machine when it’s just a lube mistake. If you’re in the market for a Mill-Turn, or you want to optimize your existing one’s lubrication setup, reach out to us to chat through your needs. We’re not just machine suppliers—we’re here to help you keep your shop running.
Aluminum Cnc Machine References:
- Modern Machine Shop. (2022). Lubrication Best Practices for Multi-Tasking Machine Tools.
- SKF Group. (2021). Grease Selection for High-Speed Machine Tool Spindles.
- ISO 12904:2018. Machine Tools – Lubricants for Machine Tools – Classification and Requirements.
- Makino Engineering Team. (2020). Maintenance Guidelines for Mill-Turn Hybrid Systems.
- Vickers Machine Tool. (2019). Contamination Control in Linear Motion Lubrication Circuits.
Smartech Machinery & Equipment Co., Ltd.
As one of the most professional mill-turn machine machine manufacturers and suppliers in China, we also support customized service. Please rest assured to buy bulk mill-turn machine machine made in China here from our factory. Contact us for more details.
Address: Room 2832, Changping Commercial Mansion, Shihua Road, Futian Free Trade Zone, Shenzhen, China
E-mail: smartech@smartechcnc.cn
WebSite: https://www.smartech-cnc.com/
